Steel products can look sound while hiding weaknesses beneath a clean surface. A beam may carry the expected load, yet contain a flaw near a weld. A pipe may meet its dimensions but fail under pressure or corrosion. That is why How to test steel product performance matters to engineers, buyers, fabricators, and quality teams. Reliable testing turns assumptions into evidence.
The right checks depend on the product, its intended use, and the risks of failure. Common methods examine tensile strength, hardness, impact resistance, chemical composition, weld quality, dimensions, and corrosion behavior. Each test answers a different question. Some require laboratory equipment; others involve careful inspection with a gauge, probe, or calibrated instrument. Small details matter. A misplaced sample or poorly recorded result can weaken an otherwise sound assessment.
This guide introduces ten practical ways to evaluate steel performance and explains what each method can—and cannot—show. Standards and qualified technicians help make results more consistent, but no single test tells the whole story. It is easy to overvalue a clean report. Testing should also reflect real service conditions, including temperature, repeated loading, and exposure to moisture. The list is a starting point, not a substitute for product-specific judgment. Even experienced teams sometimes need to revisit their assumptions.
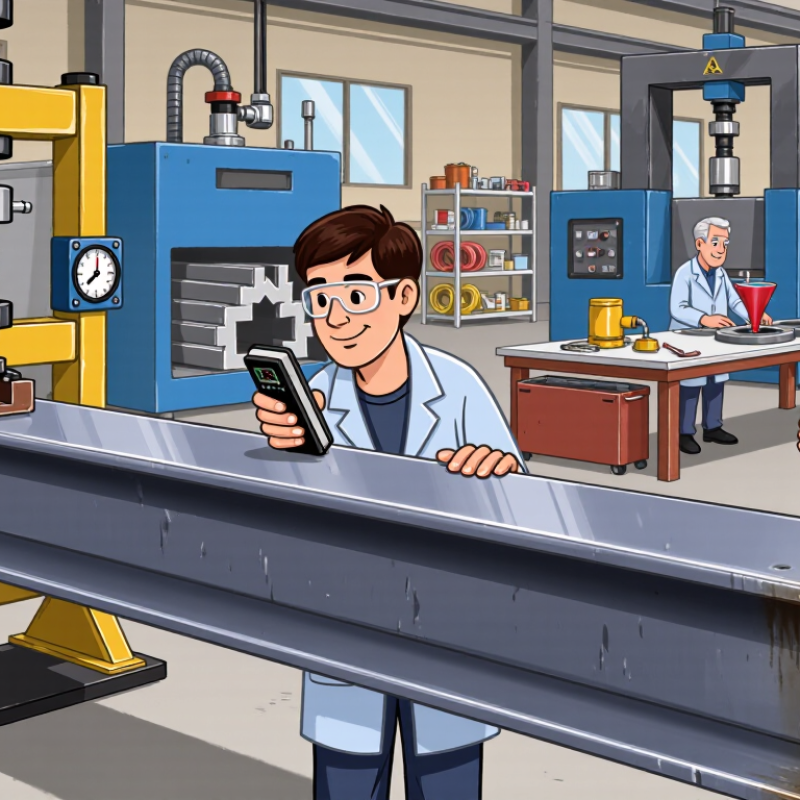
A dependable steel test begins before the specimen reaches the machine. Define the grade, product form, heat number, and governing specification first. ASTM A370 describes mechanical testing methods for steel products; it does not set every product’s acceptance limits. Those limits usually come from the applicable material specification. This distinction matters. A correct tensile result can still be judged against the wrong requirement.
Write a sampling plan that identifies the lot, specimen count, location, and retest rules. Record whether specimens come from a plate, bar, or finished component. Specify orientation: longitudinal and transverse samples may behave differently. ASTM A370 addresses specimen preparation and test procedures, while product standards may add requirements.
World Steel Association’s World Steel in Figures 2024 reports global crude steel production of 1,892.2 million tonnes in 2023. At that scale, clear traceability is practical risk control, not paperwork. Keep the heat number attached to each cut sample. A rushed label can quietly undermine good laboratory work.
Tips: Mark rolling direction on the stock before cutting. Photograph the marked surface, then log the specimen ID, dimensions, and orientation. Check that the test lab uses the requested method and reports yield strength, tensile strength, elongation, and any required bend results. If the sampling location is unclear, pause and confirm it; assumptions are easy to make, and not always easy to correct.
A tensile test turns a steel coupon into a measurable record of how it deforms under load. For a 50 mm gauge length, mark two reference points exactly 50 mm apart on the specimen’s reduced section. Measure the original diameter or width and thickness, then calculate the starting cross-sectional area. Small measurement errors matter. A scratched mark or uneven specimen edge can distort the result.
As the machine pulls the coupon, record the load and extension. Yield strength indicates when permanent deformation begins; the yield point may be gradual, so follow the chosen test method for defining it. Tensile strength is the maximum load divided by the original cross-sectional area. After fracture, fit the two pieces together and measure the distance between the marks. Elongation is the increase over 50 mm, expressed as a percentage of the original gauge length. Keep the broken ends aligned. Do not guess.
A clean result also depends on specimen preparation, machine calibration, and a steady test setup. Record the test temperature and specimen orientation, since both can affect comparisons. One limitation is easy to overlook: elongation from a 50 mm gauge length may not compare directly with results from a different gauge length. The number looks precise. Its context matters. If the fracture occurs outside the marked section, note it and assess whether the result remains valid under the applicable procedure.
Top 10 Ways to Test Steel Product Performance
Hardness testing offers a practical way to compare steel products, but results depend on the method and test conditions. Rockwell testing measures indentation depth under specified loads. It is often quick for production checks, with readings shown directly on a scale. Brinell testing presses a hard ball into the surface, then measures the indentation diameter. Its larger impression can help represent materials with uneven structures. Vickers uses a diamond pyramid and measures the impression’s diagonals, making it useful across a broad range of hardness levels and sample sizes.
Keep the comparison fair. Prepare clean, flat surfaces, and avoid testing too close to an edge or another indentation. Choose the correct scale, indenter, and load for the material and specimen thickness. A thin sheet may give misleading results if the impression reaches its back surface. Check the tester’s calibration and follow the applicable test procedure. Record the method and conditions with each reading; a number without context can cause confusion. These methods do not measure identical properties, so their values should not be treated as directly interchangeable. I’ve seen teams compare numbers too quickly. It’s an easy mistake.
Tips: Test several locations, especially when the steel may vary across its surface. Keep a simple record of readings and test conditions. If results seem inconsistent, repeat the test after checking surface preparation and setup.
The chart compares commonly used test-force settings: Rockwell major forces of 60, 100, and 150 kgf; Brinell forces of 500, 1500, and 3000 kgf; and Vickers forces of 1, 10, and 30 kgf. These are representative settings, not a complete list. Test force depends on the material, specimen thickness, and applicable procedure. Hardness values from different methods use different scales and should not be compared directly without an appropriate conversion standard.
A 10 × 10 mm Charpy V-notch specimen gives impact testing a consistent starting point. The standard geometry is specified in ISO 148-1:2016 and ASTM E23, which describe specimen preparation and pendulum-test procedures. The V-notch is typically 2 mm deep, with a 45-degree angle and a 0.25 mm root radius. Small details matter. A blunt notch or rough surface can alter crack initiation and scatter the readings.
During a test, a pendulum strikes the notched bar, and the absorbed energy is recorded in joules. Test temperature must be controlled because many steels lose toughness as temperatures fall. ASTM E23 notes that machine verification and specimen dimensions are essential to reliable results; a number without those checks can mislead. Compare specimens tested at the same temperature and orientation, and report individual values alongside the average. That is useful in practice. It is easy to overlook.
Charpy energy is not a direct prediction of service life. It is a comparative indicator, not a guarantee against fracture. For thicker products, welds, or critical structures, pair it with other evidence, such as tensile testing or fracture-toughness assessment. Even careful labs see scatter. That uncertainty deserves attention, not concealment.
Top 10 Ways to Test Steel Product Performance
Steel can pass a tensile test and still fail in service. Check corrosion resistance, weldability, and microstructure against the product specification, not assumptions. The NACE IMPACT study estimated global corrosion costs at US$2.5 trillion annually, or 3.4% of global GDP. It also estimated that applying existing corrosion-control practices could save 15–35% of those costs. That is a strong reason to test surface condition, coating integrity, and corrosion behavior in the intended environment. Use a documented method, such as ASTM G31 for laboratory immersion testing, and record exposure time, solution, temperature, and mass loss. A salt-spray result alone may not predict years outdoors.
For weldability, review the steel’s chemistry and calculate its carbon equivalent using the formula specified by the relevant standard. Then assess the actual welding procedure, including heat input, preheat, and joint thickness. Inspect welds visually and use suitable nondestructive or destructive examinations. Microstructure checks add context: metallography can reveal grain size, inclusions, decarburization, or heat-affected-zone changes. ASTM E112 provides methods for determining average grain size. One polished section is not the whole story.
Tips: Keep samples traceable to heat and batch numbers. Photograph corrosion spots and weld defects beside a scale. Compare every result with the purchase specification and acceptance limits. If results conflict, pause before release; sampling may be the weak link.
Identify the steel grade, product form, heat number, and applicable specification. ASTM A370 describes test methods, but product specifications usually set acceptance limits.
Record the lot, specimen count, sampling location, and retest rules. Note whether each sample came from plate, bar, or a finished component.
Longitudinal and transverse specimens can behave differently. Mark the direction before cutting, then photograph and record each specimen’s orientation.
Mark two points 50 mm apart on the reduced section. After fracture, fit the pieces together and measure the distance between the marks.
Gauge length affects the result. A reading from 50 mm may not match one from a different gauge length. Context matters.
It is the maximum load divided by the specimen’s original cross-sectional area. Record dimensions carefully; small errors can change the result.
They use different indenters and measurement methods. Their values are not directly interchangeable, so record the method and test conditions.
A rough surface, incorrect load, poor calibration, or testing too close to an edge can affect results. Thin samples may also be influenced by their back surface.
Include specimen identification and orientation, test conditions, and required results such as yield strength, tensile strength, elongation, or bend results. A label error can undermine otherwise careful work.
How to test steel product performance begins with identifying the correct steel grade, selecting representative samples, and following an appropriate sampling plan and test direction under ASTM A370. Tensile testing then helps assess yield strength, ultimate tensile strength, and elongation, with elongation measured over a 50 mm gauge length. Hardness can be compared using Rockwell, Brinell, and Vickers methods, chosen to suit the material and product form.
For toughness evaluation, Charpy impact testing uses standard 10 × 10 mm V-notch specimens under specified conditions. A complete assessment also verifies corrosion resistance, weldability, and microstructure against the relevant product specifications. Together, these tests provide a practical picture of a steel product’s mechanical behavior, consistency, and suitability for its intended application.
Campfire Steel